 English
 русский
The sub gate of the plastic injection mold runner system
In order to get the best injection quality, the gate type must be selected carefully, the coommon gate tyeps are: direct gate, side gate, pin-point gate, sub gate,valve gate of hot runner etc. Among them, the side gate is divided into tab gate, ear protection gate, fan gate, thin gate and so on, the sub gate is divided into sub gate, banana gate, downturning gate and so on.
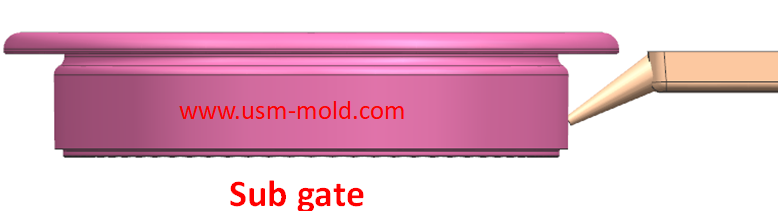
Picture 1a
According to the production automation, it is divided into manual removal and automatic removal, the side gate and direct gate are need to be manually removed after production,but the sub gate and pin-point gate and valve gate of hot runner are automatic removed.
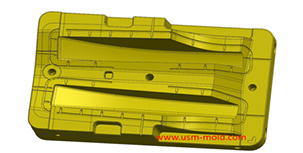
Sub gate: The sub gate is evolved from pin-point gate and has a similar characteristic as pin-point gate, the difference is that the sub gate in one side of parting surface and enters the cavity in an oblique direction. Opening the mold elbow can automatically pull off the gate, and the gate position can be set on the side, end and back of the plastic part, so that there is no gate mark on the outer surface of the plastic part (as shown in picture 1ab), the structure of the same elbow mold can be simplified to a single parting surface structure.
Picture 1b
Advantages:
1. The gate can be cut off automatically, eliminating the need for subsequent processing and realizing automatic production;
2. The gate position selection is big, it can be set freely on the outside or inside of the part;
3. The gate is small, which has little effect on the appearance of the product, and some sub gates are hard to see with the eyes;
4. The mold structure can be simplified, for some products with high appearance requirements, we must make a three-plate mold to realize it if we use the pin-point gate, but it only two-plate mold is needed if changing to sub gate, which reduces the mold structure complexity greatly, it also reduces the mold thickness and save the mold cost.
Disadvantages:
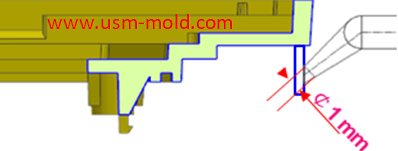
1. Pressure loss too much, it ususall in the range of Ø0.8~2.0mm due to the sub gate is relatively small, a large part of the pressure will be lost when the plastic pass through the small gate;
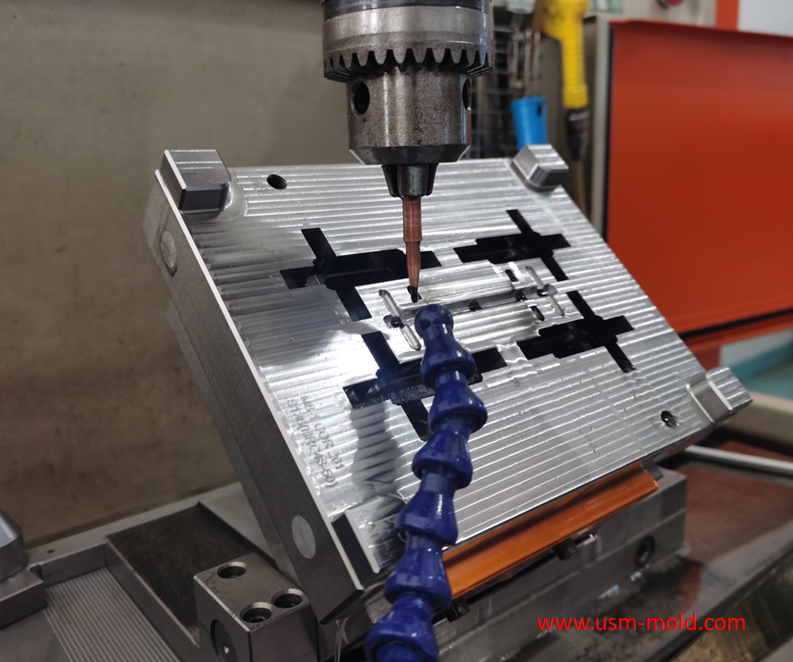
2. The processing is more complicated, this kind of small gate generally needs to place the mold core into a vertical angle to follow the gate, and then use EDM to make process(as shown in picture 2);
_20250310164515A048.webp "Voice Operated Switch Mold")
The design principle of the exhaust slot
Mar 6, 2022The exhaust system of plastic molds is also very important, if the product has air trapping or exhaust system is not suitable will have a big impact on injection molding production and product...view
The principle of mold temperature balance in plastic mold cooling system design
Feb 21, 2022The principle of mold temperature balance: 1. Due to the complexity of the plastic parts and mold structure, it is difficult to make the temperature of the mold completely consistent, but should be...view
The air trapping position in cavity and exhaust method
Mar 2, 2022The air trapping in cavity is usually in the following places: 1. Thin-wall structure cavity, the end of melt flow; 2. The junction of two or more melts; 3. The last area where the melt in the cavity...view_20250317091228A019.jpg)
Main application of gas-assisted molding technology
Apr 7, 2022Gas-assisted molding has a particularly obvious effect on the material saving of tubular and rod-shaped plastic parts, such as car handles, seat armrests, window frames, and wood-like furniture, the...view
Plastic part ribs desigining
Jan 4, 2022The ribs function: The role of ribs is to improve the strength and rigidity of the plastic parts, prevent the plastic parts from being distorted and deformed, and will not cause the appearance of the...view
Gas-assisted injection molding product defects and solutions
Apr 28, 2022Common defects and solutions of gas-assisted injection moulding: 1. Gas blows out the melt like in picture 1. Reason: insufficient pre-filled amount. When the plastic part is a locally thickened...view