 English
 русский
Slider designing tips 1
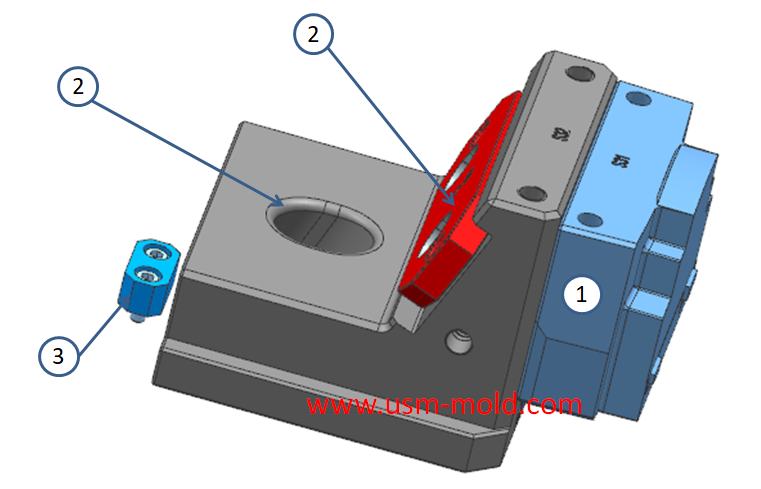
1. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially lengthened;
2. In principle, the length of the sliding part of the slider should be bigger than 1.5 times the height of the slider;
3. The mating surface of the cross-section surface of the slider going deep into the fixed die is made into a side slope of 3~5° to avoid air or unilateral, as shown in 1 in picture 1;
4. The maximum angle of the angle pin shall not exceed 22°,, and the wedge angle of the slider is 2-3° larger than that of the angle pin;
5. The entrance of the angle pin hole of the slider should be made into an R angle, as shown in 2 in picture 1;
6. The matching gap between the angle pin hole of the slider and the angle pin should be avoided by 0.5-1.0mm on one side;
7. After the slider is pulled out, there must be a stroke switch, and the slider limit device with a compression spring and a stop is preferred, as shown in 3 in picture 1;
8. A wear plate is required for the locking part of the slider, as shown in 4 in picture 1, the slider and the top of the entrance of the locking block make an R angle.
Plastic injection mold heating
Feb 16, 2022When the plastic injection molding process requires the mold temperature to be above 80°C, a temperature adjustment system with heating function must be provided in the mold. In addition,...view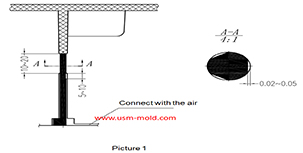
Insert pin of vengting design for molded parts
Mar 20, 2022Insert pin of venting: It is difficult to make exhaust slot when end runner is not in parting surface during injection, and there is no matching gap available, but we could make the venting pin at end...view
Plastic injection mold common cooling gate
Feb 17, 20221. Straight-through cooling water gate: the straight-through cooling gate is the most commonly used gate for plastic injection mold, and it is also the most convenient type of cooling for processing....view