 English
 русский
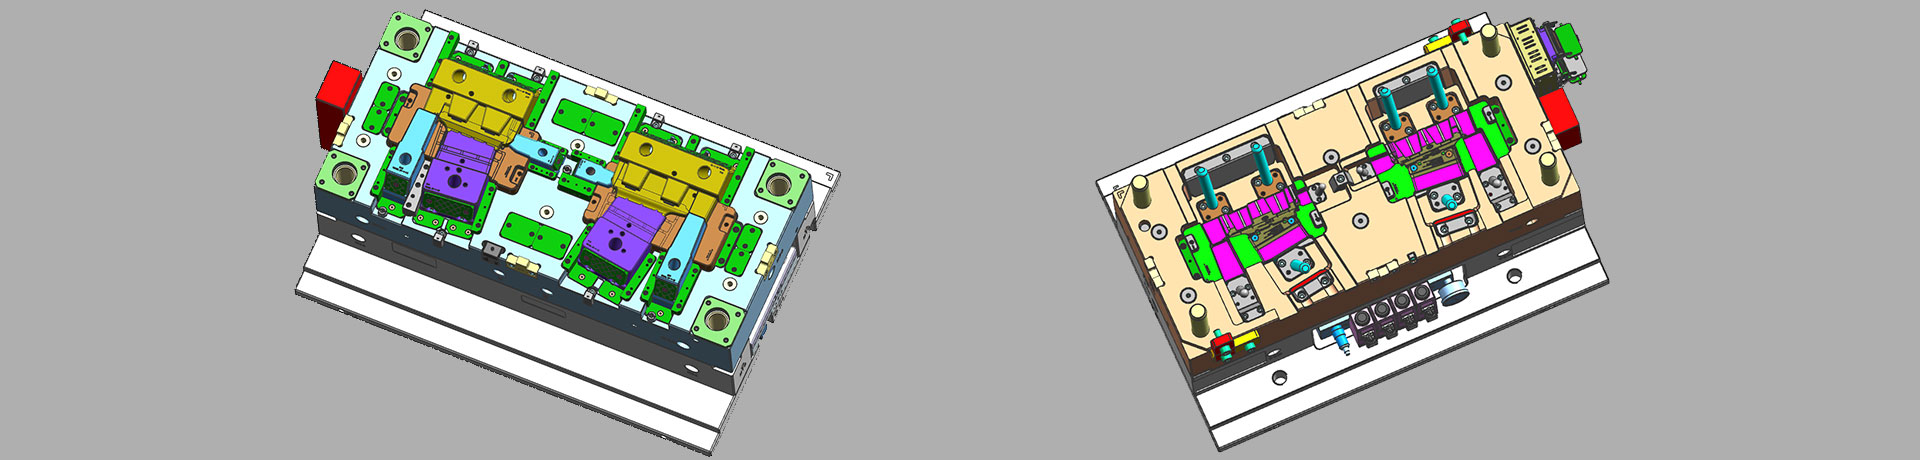
The design principle of the exhaust slot
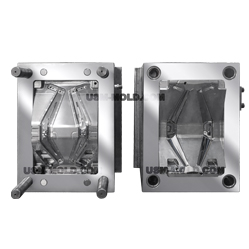
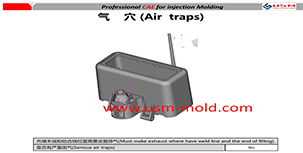
The exhaust system of plastic molds is also very important, if the product has air trapping or exhaust system is not suitable will have a big impact on injection molding production and product quality, especially for predeformation mold, the part size will be different if there is air trapping inside mold, which will cause instability during production.
We must follow the following principles when making the mold exhaust slot:
1. The exhaust must be rapid and complete, and the exhaust speed should be compatible with the filling speed;
2. The exhaust slot (hole) should be made in thicker wall thickness of the plastic part;
3. The exhaust slot should be made in parting surface as much as possible, and it is better to make it on the side of the cavity side(according to the shape, characteristics and mold structure of the plastic part, the position of the exhaust slot is allowed to make in core side);
4. The burrs generated by the overflow of the exhaust slot should not hinder the demolding;
5. The exhaust slot should be made as far as possible at the end of the material flow, such as the end of the runner and slug well ;
6. The exhaust direction of the exhaust slot should be toward the reverse operation surface;
7. Refer to the standard data for the depth of the exhaust slot and the depth of the overflow slot, the width and distance, etc.;
8. The exhaust slot should be polished along the exhaust direction;
9. Exhaust slot must be made at the weld mark area;
10. It is better to make the exhaut slot as deep as possible which can not see the flash, but it will be better to see the flash in runner area.
Reasons for making the exhaust system of the injection mold
Feb 28, 2022The gas in the injection mold includes not only the air in the cavity, but also the air in the gate and the decomposition gas generated by the plastic melt, and the steam which caused by plastic in...view
The principle of mold temperature balance in plastic mold cooling system design
Feb 21, 2022The principle of mold temperature balance: 1. Due to the complexity of the plastic parts and mold structure, it is difficult to make the temperature of the mold completely consistent, but should be...view
Design Tips of Vacuum Venting Mold
Mar 30, 2022There are some regular venting way which are parting surface venting, insert venting, insert pin venting and well-ventilated steel, but there is a special way is vacumm venting, it will need vacumm...view
Comparison of water-assisted and gas-assisted injection molding
May 19, 2022Comparing with water-assisted injection molding technology and gas-assisted injection molding technology, the fundamental difference is the nature of the auxiliary molding media used. One is liquid...view
Design principles for wall thickness of plastic products
Jan 3, 2022The principles of wall thickness design for plastic parts are as follows: 1. Making the wall thickness even is the first principle of plastic part design, it can make filling, cooling and shrinking...view
The design requirements of slider wear plate
Jan 2, 20241. The wear plate of slider requires hardening treatment, with a hardness of 45-48HRC; 2. The friction surface of the wear plate is required to be 1.0mm higher than the slider surface (see picture-1);...view