 English
 русский
Well-ventilated steel of venting design for molded parts
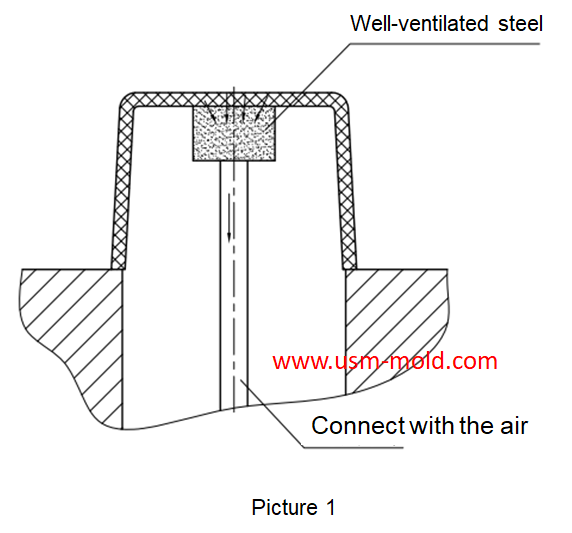
Well-ventilated steel is a sintered alloy, iIt is a porous material sintered with spherical particle alloys, the pore size is 7-10μm and the strength is poor, but the texture is loose which allow the gas to pass through. Placing a piece of well-ventilated steel on the part that needs to be vented can make venting well. However, the diameter of the bottom vent hole should not be too big to prevent it from being squeezed and deformed by the cavity pressure, due to the low thermal conductivity of well-ventilated steelsteel, it cannot be overheated, otherwise, it is easy to cause decomposition products to block the pores.
Features of well-ventilated steel:
1. The density is small and the specific strength is big.
2. Good energy absorption.
3. Good vibration damping effect.
4. Large specific surface area, a quarter of the tissue is through holes.
5. Original hardness of well-ventilated steel: pre-hardened to 350~400HV (35~40HRC).
Well-ventilated steel characteristics:
1. Reduce injection pressure and pressure holding time;
2. Reduce and eliminate the internal stress of the molded parts to prevent the deformation and warpage of the product;
3. It can solve and alleviate the difficult forming issues due to gate deviation, uneven wall thickness, and thin wall plastic parts.
4. The gas generated by the high temperature of the molding material and the defects such as scorching, flow marks, material shortage, and part deformation caused by rapid pressure accumulation in the mold cavity can be fully resolved;
5. Improve molding production efficiency and save production costs, so put well-ventilated steel in suitable place of the injection mold, the injection issue caused by the gas can be completely eliminated, making the molding process much better.
Making the well-ventilated steel tips:
1. Use H7/m6 to fix the well-ventilated steel with mold;
2. Milling, grinding, polishing, knocking, etc. are not allowed on the surface of the well-ventilated steel to avoid clogging of the vent holes, only make EDM;
3. Choose to install the well-ventilated steel in a flat position to avoid cutting;
4. Exhaust slot or vent holes must be opened on the bottom surface of the well-ventilated steel, and connect with the air;
5. The use of well-ventilated steel for exhaust air will leave the shape of ventilating micropores on the surface of the product, so the ventilating element can only be installed on the non-critical surface;
6. In order to prevent clogging of the ventilation holes, regular maintenance of the exhaust components is required during forming and production;
7. Breathable steel exhaust is not suitable for resins that require high-pressure injection molding, such as PC, PC+ABS, etc.; high-pressure injection molding will cause damage to the exhaust components
_20250310164515A048.webp "PLC Controller Shell Mold")
Slider designing tips 1
Aug 3, 20221. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially...view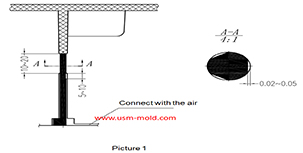
Insert pin of vengting design for molded parts
Mar 20, 2022Insert pin of venting: It is difficult to make exhaust slot when end runner is not in parting surface during injection, and there is no matching gap available, but we could make the venting pin at end...view
Design Tips of Vacuum Venting Mold
Mar 30, 2022There are some regular venting way which are parting surface venting, insert venting, insert pin venting and well-ventilated steel, but there is a special way is vacumm venting, it will need vacumm...view_20250317091113A018.jpg)
The basic points of designing gas-assisted injection molding
Apr 17, 20221. Firstly, considering the suitable wall thickness areas needs to be injected and hollowed out, and then decide how to connect them with the gas channel; 2. The gas channel should be arranged in...view
USM Blogo Opening
Oct 27, 2021Hello everyone! Our blog is open today, it is very glad to have the opportunity to meet you here, welcome to visit us whenever you need. USM is a professional plastic injection mold and molding...view
Water assisted injection molding introduction
May 11, 2022Like the gas-assisted injection molding process, water-assisted injection molding injects a piece of plastic into the mold cavity and core firstly, and then injects water to squeeze the melt plastic...view