 English
 русский
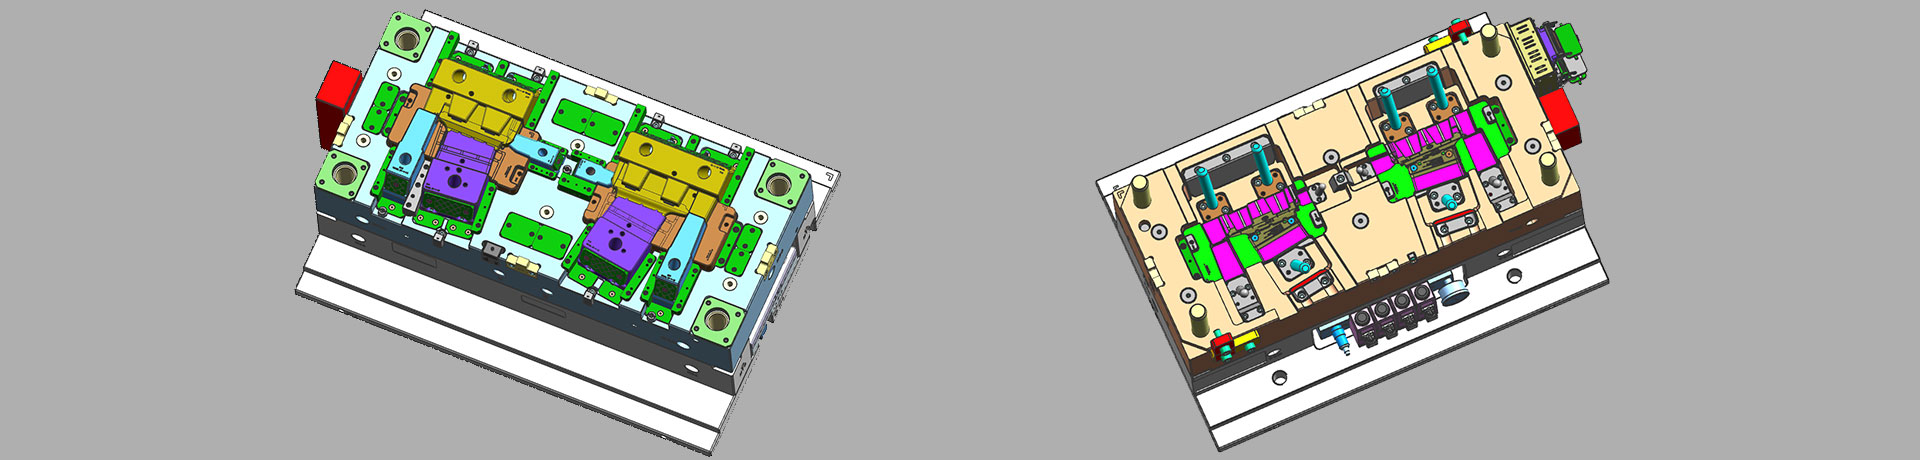
Slider designing tips 2
9. The molding parting surface of the slider molding should be made as a shut-off surface as possible, and the width of the shut-off part should be at least 8mm, and do not make a shut-off surface;
10. When using the center guide slider, we should follow the company standard "slide center guide slider design" strictly;
11. When the mold is closed, if there is a risk of interference between the slider and other parts, the reset mechanism must be done first;
12. The core-pulling distance of the slider must be bigger than the actual core-pulling distance of the product by 3-5mm;
13. The large slider should be avoided to be set in the direction of the top side of the mold as far as possible; if it is unavoidable, it should be driven by an hydralic cylinder, and a stroke switch should be installed to cooperate with it;
14. When the cylinder core-pulling device is not used for the slider on the day side, the strength of the slider limit device must be checked to ensure that the weight of the slider does not exceed 2/3 of the strength of the limit device to prevent accidents;
15. When the slider is set on the ground side, the spring can be cancelled, but at the same time, a reliable stop should be designed to prevent the slider from falling off due to its own weight;
16. The same material cannot be used if there is frictional movement between the parts or the requirements of the insertion.
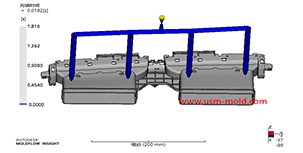
Plastic injection mold runner system design points
Jan 9, 2022When designing the gating system, Firstly, we should consider making the plastic melt fill the cavity with core side quickly to reduce pressure and heat loss; secondly, it should be economically...view
The air trapping position in cavity and exhaust method
Mar 2, 2022The air trapping in cavity is usually in the following places: 1. Thin-wall structure cavity, the end of melt flow; 2. The junction of two or more melts; 3. The last area where the melt in the cavity...view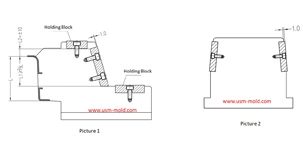
The design requirements of slider wear plate
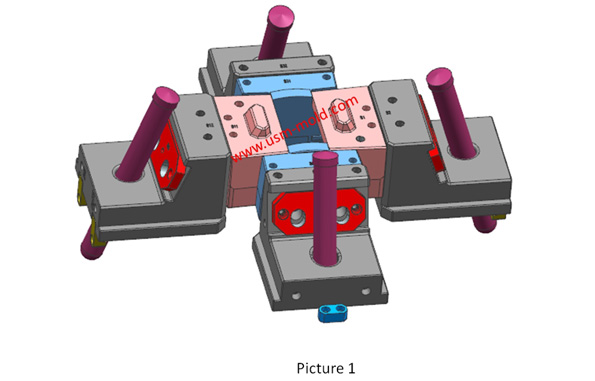
Jan 2, 20241. The wear plate of slider requires hardening treatment, with a hardness of 45-48HRC; 2. The friction surface of the wear plate is required to be 1.0mm higher than the slider surface (see picture-1);...view
Key points of gas-assisted injection molding process
Apr 20, 2022Gas injection parameters The gas-assisted control part is a device that controls the gas pressure in each stage, the gas-assisted parameters have only two values: gas injection time (seconds) and gas...view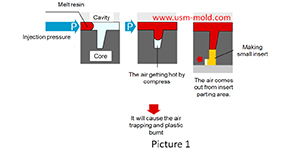
The main reasons for air trapping of plastic injecton mold
Mar 1, 2022During the injection molding process, the front end of the slight ribs may be air trapped and plastic burnt, and also cause the molded part may become black and carbonized. The mechanism of air...view
Design Tips of Vacuum Venting Mold
Mar 30, 2022There are some regular venting way which are parting surface venting, insert venting, insert pin venting and well-ventilated steel, but there is a special way is vacumm venting, it will need vacumm...view