 English
 русский
Main application of gas-assisted molding technology
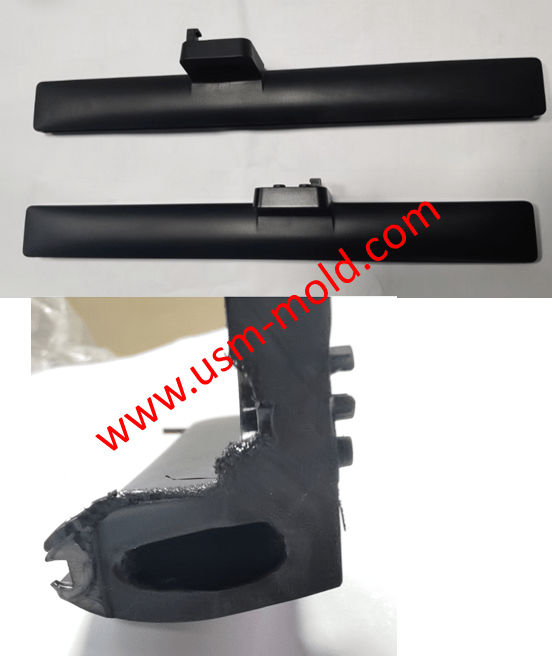
Gas-assisted molding has a particularly obvious effect on the material saving of tubular and rod-shaped plastic parts, such as car handles, seat armrests, window frames, and wood-like furniture, the material saving rate of this kind of parts can be reached in 20%-40%. For large flat parts, such as door panels, refrigerator trays, automotive interior and exterior parts, gas-assisted reinforcing ribs can be used to eliminate the warping deformation of the flat parts due to residual stress and improve the strength of the parts. Home appliances are the largest application field of gas-assisted technology., for large-screen color TVs and TV brackets over 64cm, more than 90% of them use gas-assisted molding technology, with the increasing market demand for large-screen color TVs and cars, and the popularization of home computers, gas-assisted molding technology will obtain immeasurable economic benefits in the application of household appliances. From the perspective of the trend of replacing steel with plastic, the automobile, furniture, construction, and instrumentation industries will also compete to use gas-assisted molding technology in order to save materials, improve product quality, and participate in the competition in the international market. The promotion and application of gas-assisted molding technology has pushed the plastics processing industry to a new stage of development.
_20250310164515A048.webp "Voice Operated Switch Mold")
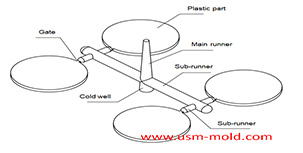
Design principles of plastic injection mold runner system
Jan 6, 20221. Quality first The design of the gating system has a big influence on part quality, firstly the gate should be set at the easiest part of the plastic part to be removed, and at the same time, the...view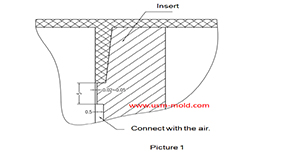
Venting insert design of molded parts
Mar 13, 2022In the thin-walled cavity, the end of the melt flow, the bottom of the blind hole of the mold cavity, the end of the solid column of the plastic part, the bottom of the plastic part rib and screw...view
Slider designing tips 1
Aug 3, 20221. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially...view
The air trapping position in cavity and exhaust method
Mar 2, 2022The air trapping in cavity is usually in the following places: 1. Thin-wall structure cavity, the end of melt flow; 2. The junction of two or more melts; 3. The last area where the melt in the cavity...view
Design principle of plastic injection mold cooling system
Feb 13, 2022Design principle of cooling system In order to improve the efficiency of the cooling system and make the cavity surface temperature distribution even, the following principles should be followed in...view
Gate position determination of plastic injection mold runner design system
Jan 17, 2022In the selection of gate location, the following issues should be paid attention to: 1. The gate position should be set at the maximum wall thickness of the plastic part, so that the plastic melt...view