 English
 русский
Venting of parting surface
The exhaust slot on the parting surface is easy to clean and processing, also not easy to be blocked, and has a good exhaust effect, it is the main area where the gas is exhausted, so the exhaust from the parting surface is very popular by injection mold factory and injection molding plant. If the parting surface is curved or inclined, CNC machining, electrode processing or wire cutting is generally used, the roughness of the parting surface after processing is relatively high, Ra is generally 1.6~6.3μm, and the exhaust slot is generally processed directly by CNC. If the parting surface is flat, it is usually processed by a grinding. The roughness of the parting surface after the grinding machine is low, Ra is 0.2~0.8 μm, the parting surface is tightly fitted, and the gas in the cavity is not easy to discharge. In this case, an exhaust slot must be opened on the parting surface on one side of the cavity. There are two ways to open the exhaust slot on the parting surface: one is to open the exhaust slot locally, and the other is to open the exhaust slot around the part.
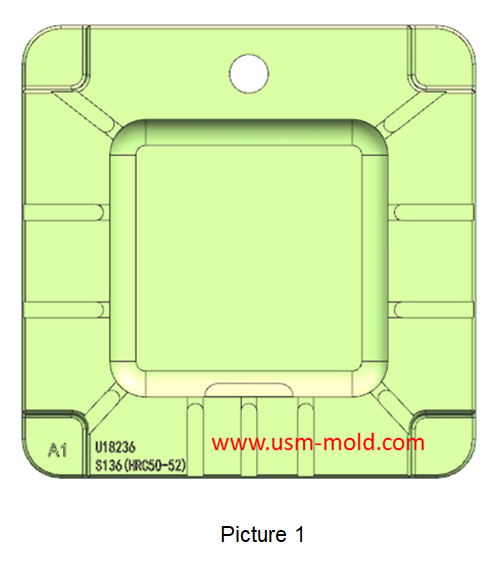
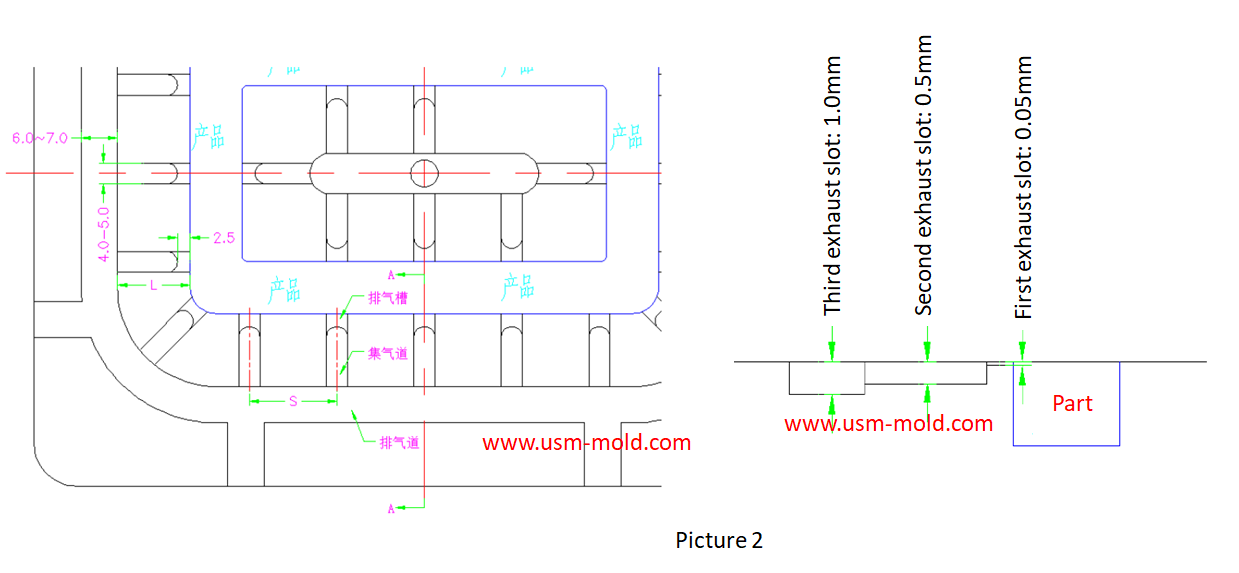
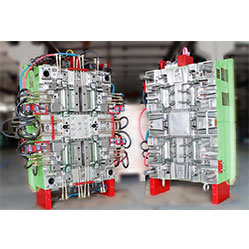
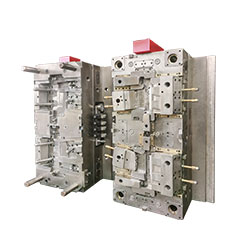
1.Parting surface with partial exhaust slot: this is the most commonly used method of exhaust, the method is to open the exhaust slot where the air is trapped. The position of the exhaust slot is generally combined with the mold flow analysis report based on experience. Determine its final trapped position. This type of venting has less damage to the parting surface of the mold, and it is more flexible and convenient to change the back mold, the specific form is shown in picture 2.
2. Exhaust slot are opened around the parting surface: when the air trap is particularly serious, a large area of exhaust slot can be used to exhaust, as shown in picture 2. If the parting surface of this kind of exhaust slot is flat, it is usually processed with a flat-bottom milling cutter. If the parting surface is curved, it is usually processed with an R-shaped ball cutter, this type of exhaust slot is divided into a first-level exhaust slot, a second-level exhaust slot and a third-level exhaust slot, the depth of which is different.
_20250310164515A048.webp "Touch Switch Sensor Mold")
What is the side parting and core pulling mechanisms with their function?
May 31, 2022When there are holes, cavities or cores on the inside or outside of the injection-molded plastic parts that are different from the opening and closing directions of the mold, the plastic parts cannot...view
Plastic injection mold runner system design points
Jan 9, 2022When designing the gating system, Firstly, we should consider making the plastic melt fill the cavity with core side quickly to reduce pressure and heat loss; secondly, it should be economically...view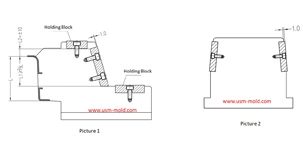
The design requirements of slider wear plate
Jan 2, 20241. The wear plate of slider requires hardening treatment, with a hardness of 45-48HRC; 2. The friction surface of the wear plate is required to be 1.0mm higher than the slider surface (see picture-1);...view