 English
 русский
Factors affecting the cooling rate of parts by injection molding
It should be shaped by cooling to get stable plastic part after plastic filling the cavity and core side, so most injection molds need to be equipped with cooling devices to make the mold temperature meet the requirements of the molding process. For plastics with high viscosity and poor fluidity, it is necessary to increase the heating temperature and add heating devices in case of difficult molding, due to the low mold temperature.
Importance of mold temperature control system
The mold temperature control and adjustment system affects the quality directly, molding and production efficiency of the part. If the surface temperature of the cavity and core is too high, it is easy to cause flash at the clamping part, and the wall thickness of the plastic part is easy to shrink; if the cavity temperature is too low, it is easy to have defects such as poor filling and insufficient strength at the weld line of the plastic part. If the surface temperature of the cavity and core is uneven, and the temperature difference is large, internal stress will be generated in the molded plastic part, resulting in warpage and deformation after molding, so the mold temperature control system is as important as the gating system, and it is also one of the key to mold design, the design of mold temperature control system should be very careful.
Whether the mold temperature is reasonable is related to the dimensional accuracy, appearance and internal quality of the molded plastic parts, as well as the production efficiency of the plastic parts, so it is an important job in the mold design. Different types of plastics have different temperature requirements for the mold, the general requirement is to make the mold temperature meet the requirements of the process conditions suitable for product molding, and the temperature control system can be adjusted to make the temperature on each part of the mold cavity and core basically the same, the mold temperature should be balanced and consistent in each molding cycle during production process for a long time.
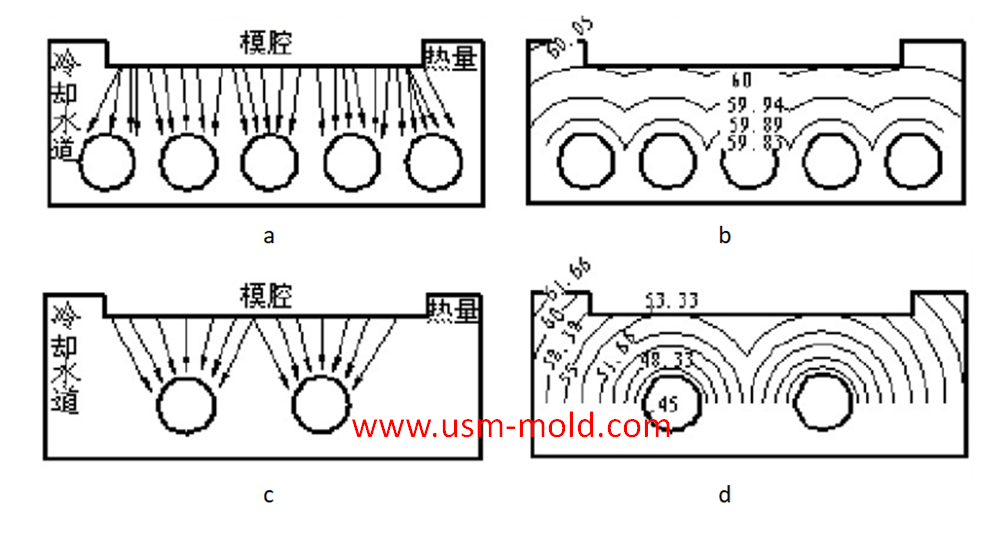
The influence of the cooling water gate of the mold temperature control system on the surface temperature of cavity and core side, the surface temperature of the cavity is relatively uneven and the change of 60~60.05 ℃ when 5 bigger cooling gate are used, it shows in following picture a and b, as shown in following picture C and d, the big temperature difference will cause uneven shrinkage, resulting in warpage and deformation.
The role of mold temperature control system
1. Improve molding performance and shorten molding cycle;
2. Stable part dimensional accuracy and prevent deformation;
3. Eliminate appearance defects and improve the surface quality of plastic parts;
4. Improve the mechanical and physical properties of the product.
_20250310164515A048.webp "Voice Operated Switch Mold")
Five Major Steps of the Injection Mold Production Process
Dec 9, 2021Injection mold manufacturing can be roughly divided into the following steps: Process analysis of plastic products. Before the mold design, the designer should fully analyze and study whether the...view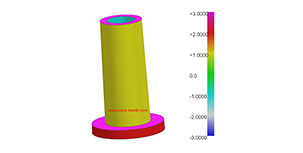
What is Called Draft Angle?
Dec 29, 2021The draft angle is also called demold angle and angle which is used for product removal from the mold and designed on the parting surface, the angle is called draft angle which shows in picture 1....view
What is the side parting and core pulling mechanisms with their function?
May 31, 2022When there are holes, cavities or cores on the inside or outside of the injection-molded plastic parts that are different from the opening and closing directions of the mold, the plastic parts cannot...view
Slider angle designing tips
Dec 4, 20231. Normally, all the insertion slopes of the slider are not allowed to be less than 3° to prevent excessive self-locking force and scratched; 2. The angle of the locking surface must be bigger than...view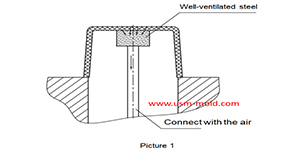
Well-ventilated steel of venting design for molded parts
Mar 14, 2022Well-ventilated steel is a sintered alloy, iIt is a porous material sintered with spherical particle alloys, the pore size is 7-10μm and the strength is poor, but the texture is loose which allow the...view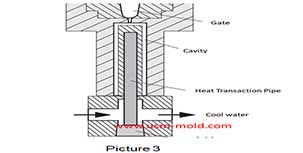
Plastic injection mold common cooling gate
Feb 17, 20221. Straight-through cooling water gate: the straight-through cooling gate is the most commonly used gate for plastic injection mold, and it is also the most convenient type of cooling for processing....view