 English
 русский
New Five-Axis CNC Machine Arrival
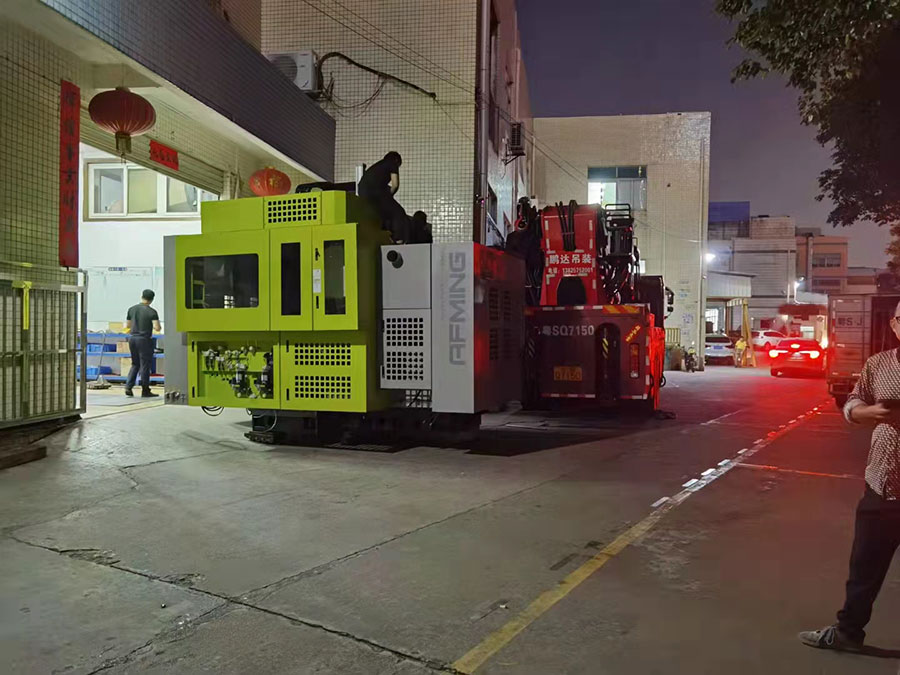
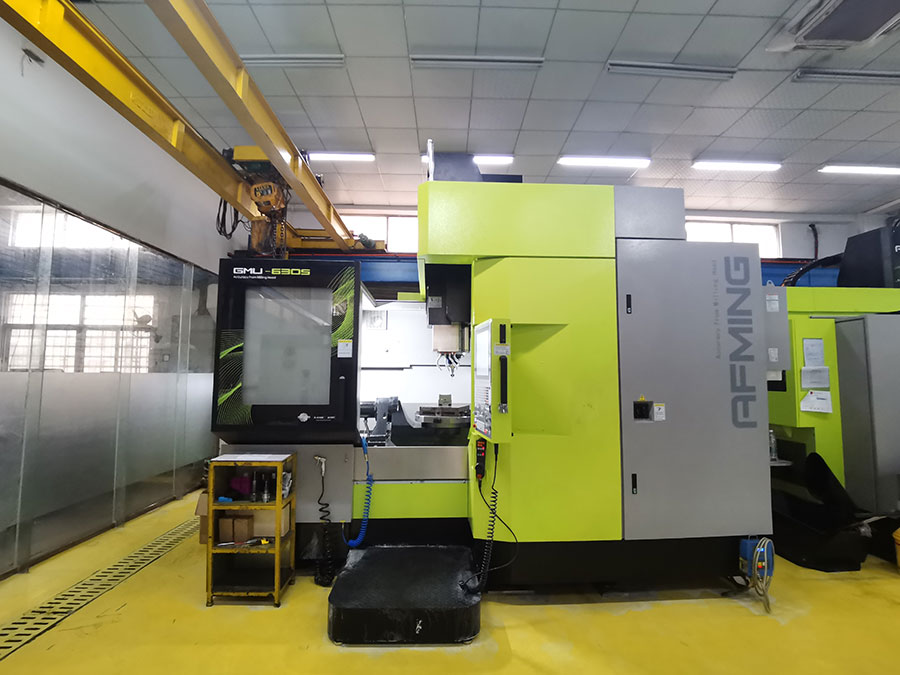
The new 5 axis CNC machining machine has arrived in our workshop on 6th Nov. 2021 and is now putting into use.
GMU-6350 type CNC machining machine
Working stroke (XYZ): 630*500*550
Maximum loading: 800kg
Machining accuracy: ±0.01mm
The rotation angle of centre worktable: 360 degree
Turning angle of centre worktable: 120 degree
Main working advantages:
1. It can process a continuous and smooth curve surface, and also can finish some parts which can not be processed by general three-axis CNC machine or are difficult to complete in one time, especially traditional three-axis machinings centres such as blades of aero engines and steam turbines, and propellers for ships, for parts that cannot be processed, the five-axis can be processed directly;
2. It can improve and control the processing accuracy and quality of curve surface;
3. Reduce clamping and changing appliques time and files ;
4. For the processing of deep cavities undercuts and small ribs on the mold, it can be processed by a five-axis machining centre to reduce electrical discharge and other processes directly, and improve the quality and efficiency of the mould.
Since USM was founded in 2011, USM has continuously improved the machine and equipment, from installation, adjustment, training of employees to putting into use, step by step to increase the production capacity and improve the quality. We always adhere to the needs of customers, and adjust the positioning of enterprises in the process of cooperation with customers, so as to achieve the goal of customer requirements, and constantly provide customers with more professional and better mold programs and services.
In the future, we will also strive to move forward, accumulate more than ten years of experience in the mold industry, and continue to create unique value for customers, USM is looking forward to providing quality service to our customers.
Design principles of plastic injection mold runner system
Jan 6, 20221. Quality first The design of the gating system has a big influence on part quality, firstly the gate should be set at the easiest part of the plastic part to be removed, and at the same time, the...view
Slider designing tips 1
Aug 3, 20221. After the slider core pulls out, the length of staying in the guide pin slot should not be less than 2/3 of the total length of the slider, for special cases, the slider slot can be partially...view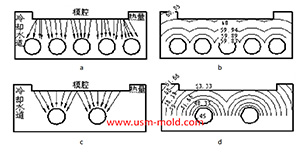
Factors affecting the cooling rate of parts by injection molding
Feb 9, 2022It should be shaped by cooling to get stable plastic part after plastic filling the cavity and core side, so most injection molds need to be equipped with cooling devices to make the mold temperature...view
Plastic injection mold runner system design points
Jan 9, 2022When designing the gating system, Firstly, we should consider making the plastic melt fill the cavity with core side quickly to reduce pressure and heat loss; secondly, it should be economically...view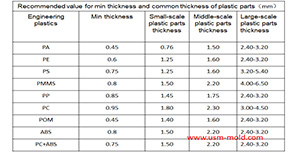
Design principles for wall thickness of plastic products
Jan 3, 2022The principles of wall thickness design for plastic parts are as follows: 1. Making the wall thickness even is the first principle of plastic part design, it can make filling, cooling and shrinking...view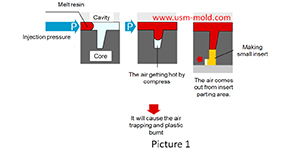
The main reasons for air trapping of plastic injecton mold
Mar 1, 2022During the injection molding process, the front end of the slight ribs may be air trapped and plastic burnt, and also cause the molded part may become black and carbonized. The mechanism of air...view